


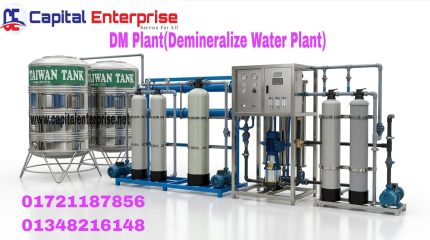
DM Plant (Demineralized Water Plant)
Industrial Applications of DM Plant (Demineralized Water)
Demineralized (DM) water is critical for industries requiring high-purity water free from minerals and ions. Using DM water protects expensive machinery, improves product quality, and ensures compliance with international standards.
Our customized DM plants serve a wide range of industrial applications:
Boiler Feed Water: Essential for power plants and textile mills. DM water prevents scaling (mineral buildup) and corrosion, drastically increasing boiler efficiency and lifespan.
Pharmaceuticals & Laboratories: Used in medicine formulation, injection preparation, and laboratory testing where 100% pure, contaminant-free water is strictly mandatory.
Textile & Dyeing Industry: Eliminates mineral interference during the dyeing process, ensuring uniform fabric coloring, precise chemical mixing, and perfect shade consistency.
Chemical & Cosmetics Manufacturing: Acts as a pure base ingredient for manufacturing chemicals, shampoos, lotions, and cosmetics, enhancing product stability and shelf life.
Electronics & Battery Production: Crucial for cleaning delicate semiconductors and circuit boards. It is also highly used as battery water to maximize the efficiency of automotive and IPS batteries.
Precision Component Washing: Used in the automobile and manufacturing sectors for spot-free rinsing of high-end machinery and precision metal parts.
📞 Contact Us Today
Get in touch with our engineering team today to configure the ideal DM Plant layout and capacity for your facility.
Mobile: 01721187856, 01348216148(Whatsapp)
Website:www.capitalenterprise.
net
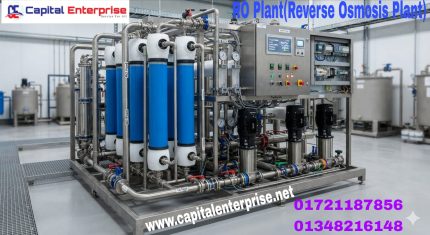
RO Plant (Reverse Osmosis Plant)
Major Applications of Reverse Osmosis(RO) Water Treatment Plants
To maintain product quality and protect heavy machinery in industries and commercial sectors, Capital Enterprise provides customized RO plants that are widely used in the following fields:
Textile & Dyeing Industry: Supplies iron-free and soft water to ensure flawless fabric color shades and premium finishing.
Pharmaceuticals & Laboratories: Guarantees 100% bacteria, virus, and TDS-free purified water required for medicine manufacturing and lab testing.
Food & Beverage: Maintains the natural taste, hygiene, and safety of water used in juice, soft drinks, and bottled water factories.
Boilers & Cooling Towers: Prevents scaling and mineral buildup inside pipelines, increasing boiler lifespan and reducing fuel costs.
Commercial Buildings & Hotels: Serves as a central water supply system in high-rise buildings, hotels, and resorts to deliver safe drinking and utility water.
Key Benefit: Using Capital Enterprise RO plants improves your final product quality, extends the lifespan of factory machinery, and significantly reduces operational expenses.
📞 Contact Us Today
Get in touch with our engineering team today to configure the ideal DM Plant layout and capacity for your facility.
Mobile: 01721187856, 01348216148(Whatsapp)
Website:www.capitalenterprise.net